Spacer Rings, Varifocal or Custom Focal Length: Choosing and Documenting an Exact FOV
Answer the field of view question with the error budget, not with whichever option is easiest to buy. If a catalog lens already produces...
read more…
Settle one question before you touch the CAD template: who moves focus, the camera or the lens. If each of the eight positions must stay interchangeable and serviceable, commit to C-mount and hold the 17.526 mm flange focal distance as a controlled drawing datum. If the package is too tight for a 25.4 mm thread, the sensor is small, and your team accepts per-unit focus setting, commit to S-mount and draw the thread, locknut, and focus-lock detail explicitly, because M12 by itself defines a thread, not an optical position. Either way, require the lens maker to deliver a revision-controlled mechanical package, measured optical data on your exact sensor at your working distance, and batch test records before the mounting drawing is locked. Those three evidence sets are what separate an interface choice from a producible eight-camera cell.
When a project calls for this format, the Lensmind M12 lens series groups the focal lengths and locking options we ship in volume.
Most comparisons of the C-mount versus S-mount lens interface for compact camera systems argue about size and price. The cleaner test is focus ownership. A C-mount interface fixes the flange focal distance at 17.526 mm, so the camera side owns a real axial datum: any compliant lens seats against a defined shoulder, and the optical position repeats from station to station. An S-mount, the M12 × 0.5 thread found on board-level modules, has no standardized flange position. Focus is set by threading the lens in and out until the image resolves, which means the lens and the assembler jointly own the focus travel.
That ownership question drives everything else in the cell. If your mechanical design already includes a way to trim sensor position, such as shimmed camera plates or an adjustable carrier, then an interface with a defined datum is attractive, and C-mount buys you interchangeability across all eight stations. If instead the lens must own focus, you are choosing an adjustment process, and the drawing has to describe it: threading procedure, locknut, thread-locking compound, and inspection after lock. Our own selection guidance follows the same split. Board-level and embedded cameras that see vibration go with M12 (S-mount) and a thread-locked focus, while 2/3-inch to 1.1-inch formats that want accessory flexibility go with C-mount. A deeper side-by-side of the two interfaces lives in our M12 versus C-mount comparison, and it is worth reading before the team argues about barrel diameters.
There is a practical sequencing benefit too. Deciding focus ownership first keeps the mounting drawing honest. When the camera owns focus, your drawing carries a seat datum and a flange window, and the lens is a replaceable commodity. When the lens owns focus, your drawing carries a process, and the lens is a qualified assembly with a named part number. Confusing the two is how cells end up with eight individually tuned cameras that nobody can service.
C-mount and CS-mount share a thread but not a reference plane: 17.526 mm versus 12.5 mm, bridged by the common 5 mm adapter ring. The flange focal distance is the number that decides whether a lens reaches focus on a given camera at all, so the margin arithmetic belongs on your drawing, not in a catalog footnote. Three questions should close before release. First, which interface does the camera actually implement? A note that says only “C/CS compatible” is underdefined, because the two positions differ by exactly the ring thickness. Second, who owns the ring? If the adapter is part of your bill of materials, its thickness tolerance joins the stack between sensor and lens seat, and your housing datum inherits that variation; if the ring ships with the camera, get its tolerance in writing. Third, where does the remaining margin go? After the ring, cover glass, and any filter stack are counted, the residual has to absorb the lens focal-length tolerance and your focus-trim budget, and the lens maker should state the acceptable sensor-to-mount distance range for the exact part number rather than leaving you to infer it from the thread.
Write the result onto the drawing as numbers: interface designation, seat datum, ring inside or outside the stack, and the permitted sensor-to-seat window. That single note prevents the most common eight-camera failure, where seven stations focus and the eighth does not because a different technician assembled it with a different ring assumption.
Evidence to request from the lens maker before finalizing the mounting design falls into three groups, and each group should arrive as revision-controlled documents tied to a specific part number, not as marketing pages or screenshots.
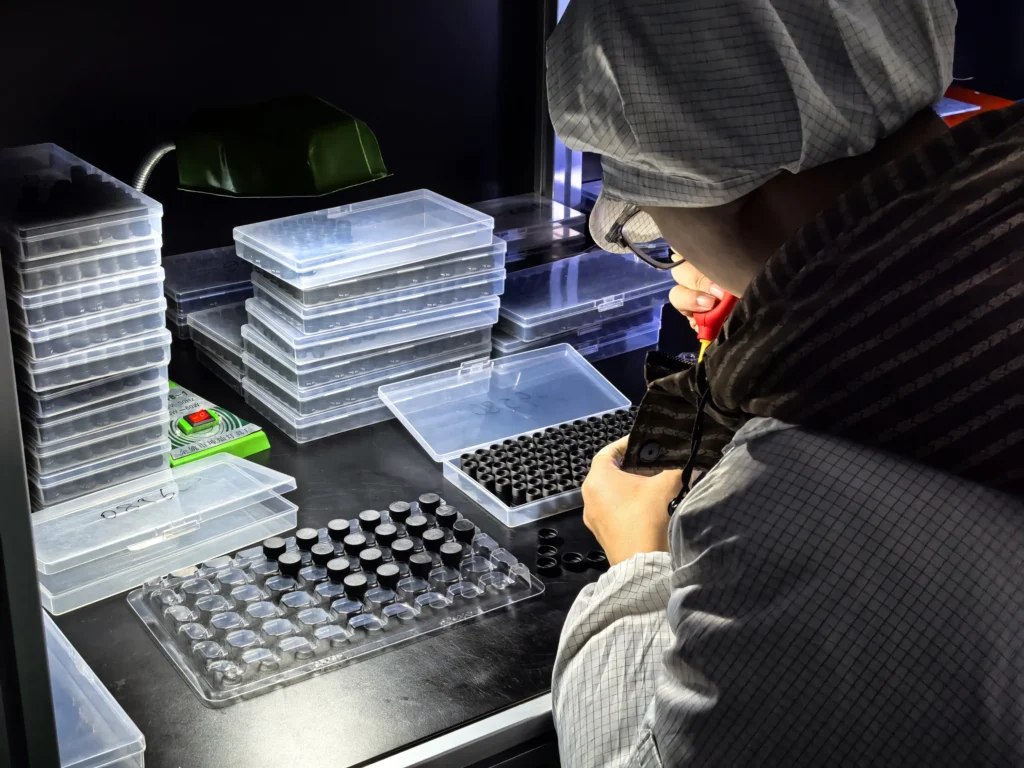
Mechanical data comes first because it is what your drawing consumes. Ask for the thread specification with tolerance and usable engagement length, the lens seating datum, the full envelope including the focus-position range, the maximum rear protrusion at the fully screwed-in condition, the recommended camera-side thread depth, locknut dimensions with permitted tightening torque, and the mass with any support requirement. For S-mount, the rear-protrusion number is the one that protects your sensor: the barrel must never reach the cover glass or filter at worst-case thread engagement, and no generic M12 callout guarantees that.
Optical data comes second, measured rather than nominal. Request image circle against your sensor diagonal, MTF at your pixel-limited spatial frequencies at center, mid-field, and corner, distortion, relative illumination, chief ray angle if your sensor is microlens-sensitive, and spectral transmission across your illumination band. Insist that these numbers are taken at your working distance and aperture, because catalog values quoted at infinity say little about a cell that images parts 65 mm away. Ask directly whether focal length and distortion are measured values or design targets, and ask for the same data on production units, not only the engineering sample.
Procedure data comes third. The maker should describe how focus is set in production, how it is locked, whether the locking step shifts focus or tilts the optical axis, which thread-locking compounds are compatible with the barrel materials, and what curing time the joint needs before handling. Add a change-control commitment covering barrel geometry, glass, and coatings, so the lens you qualify is the lens you receive in volume. This exchange fits inside a drawing week: at Lensmind, drawings move only under NDA, and custom RFQ feasibility is answered within 48 hours.
One excellent sample proves nothing about a cell of eight. The question that matters is camera-to-camera interchangeability: if a lens is replaced with another production unit, does the new one reach focus without shimming, rethreading, or recalibration? That property is demonstrated with batch records, not asserted in a meeting. Require per-batch test documentation that names the batch number, test conditions, inspection coverage, and an explicit pass or fail judgment, covering MTF, distortion, back focal length, and depth of field. These reports should be a default deliverable on every production batch, not a document you must extract from a sales engineer.
Ask the maker to state consistency capability in numbers. Our FA machine-vision line holds distortion below 0.05 percent with batch consistency demonstrated across lots above ten thousand units. Units that need it are built with 1 μm-class active alignment in a Class 10,000 cleanroom, centration is checked on Trioptics equipment, and wavefront is verified on a laser Fizeau interferometer. Numbers like these are what allow one calibration routine to serve all eight stations, and they are the difference between a supplier who measures every batch and one who measures the golden sample once.
If you go S-mount, add retention evidence to the same request: focus position after vibration and temperature cycling, whether the locknut or focus-lock feature moves the optical axis when tightened, and the recommended re-check interval after service. Our M12 families include FT and HT focus-lock options built for anti-vibration duty, and the practical failure modes, from thread creep to lock-induced axis shift, are covered in our article on M12 focus lock and vibration. Bring that document to the same review as the mounting drawing, because retention behavior is part of the interface you are committing to.
With the deadline in front of you, use this default logic. If the position is an embedded, small-sensor camera inside a vibrating cell, choose S-mount and draw the complete retention detail: thread callout with tolerance, engagement depth, locknut, anti-rotation feature, and the exact lens part number from our M12 focus-lock types. If the station runs 2/3-inch to 1.1-inch formats, needs measurement-grade distortion, or must accept telecentric or macro optics later, choose C-mount and name the lens on the drawing, for example FA3505W or FA7520W from our FA machine-vision family, together with the seat datum and the flange window.
Whatever the choice, do not release a drawing that says only “C-mount” or “M12”. Specify the exact part number or controlled optical interface, the datum scheme, maximum rear intrusion, clearances to neighboring barrels and cables, the focus-lock method, and the permitted replacement procedure. Build in slack where it is cheap now: shim capability at the camera plate, radial clearance around each barrel, and wrench access for every locknut. If a second phase or spare lenses will follow, confirm supply terms early. Our standard written commitment is prototype to mass production in 60 working days, with repeat orders in 30 days, which is usually fast enough to hold a spares plan together. Lock the numbers, archive the evidence package against the drawing revision, and the eight cameras will behave like one instrument instead of eight separate bets.

Answer the field of view question with the error budget, not with whichever option is easiest to buy. If a catalog lens already produces...
read more…
C-mount is 17.526 mm. CS-mount is 12.526 mm. Same 1-32 UN thread. The 5 mm ring is one-way.
read more…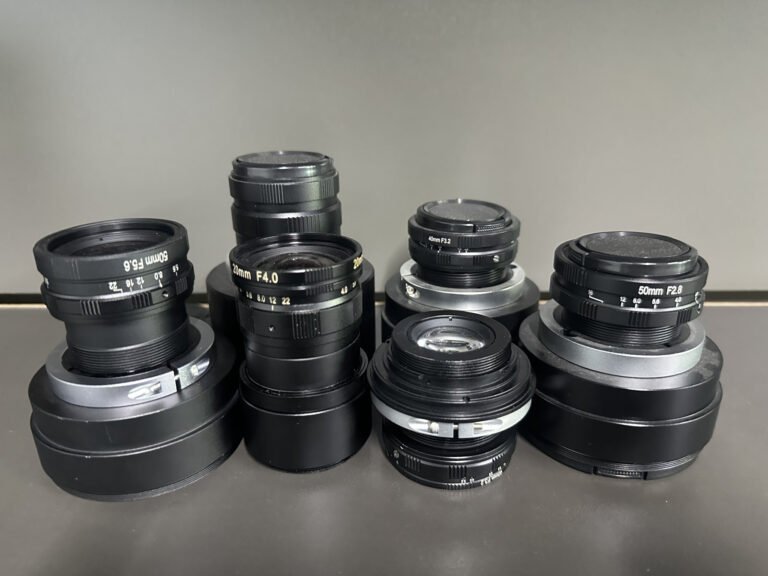
M12 is M12x0.5 with no flange standard. C-mount is 1-32 UN at 17.526 mm. Match the camera body first.
read more…